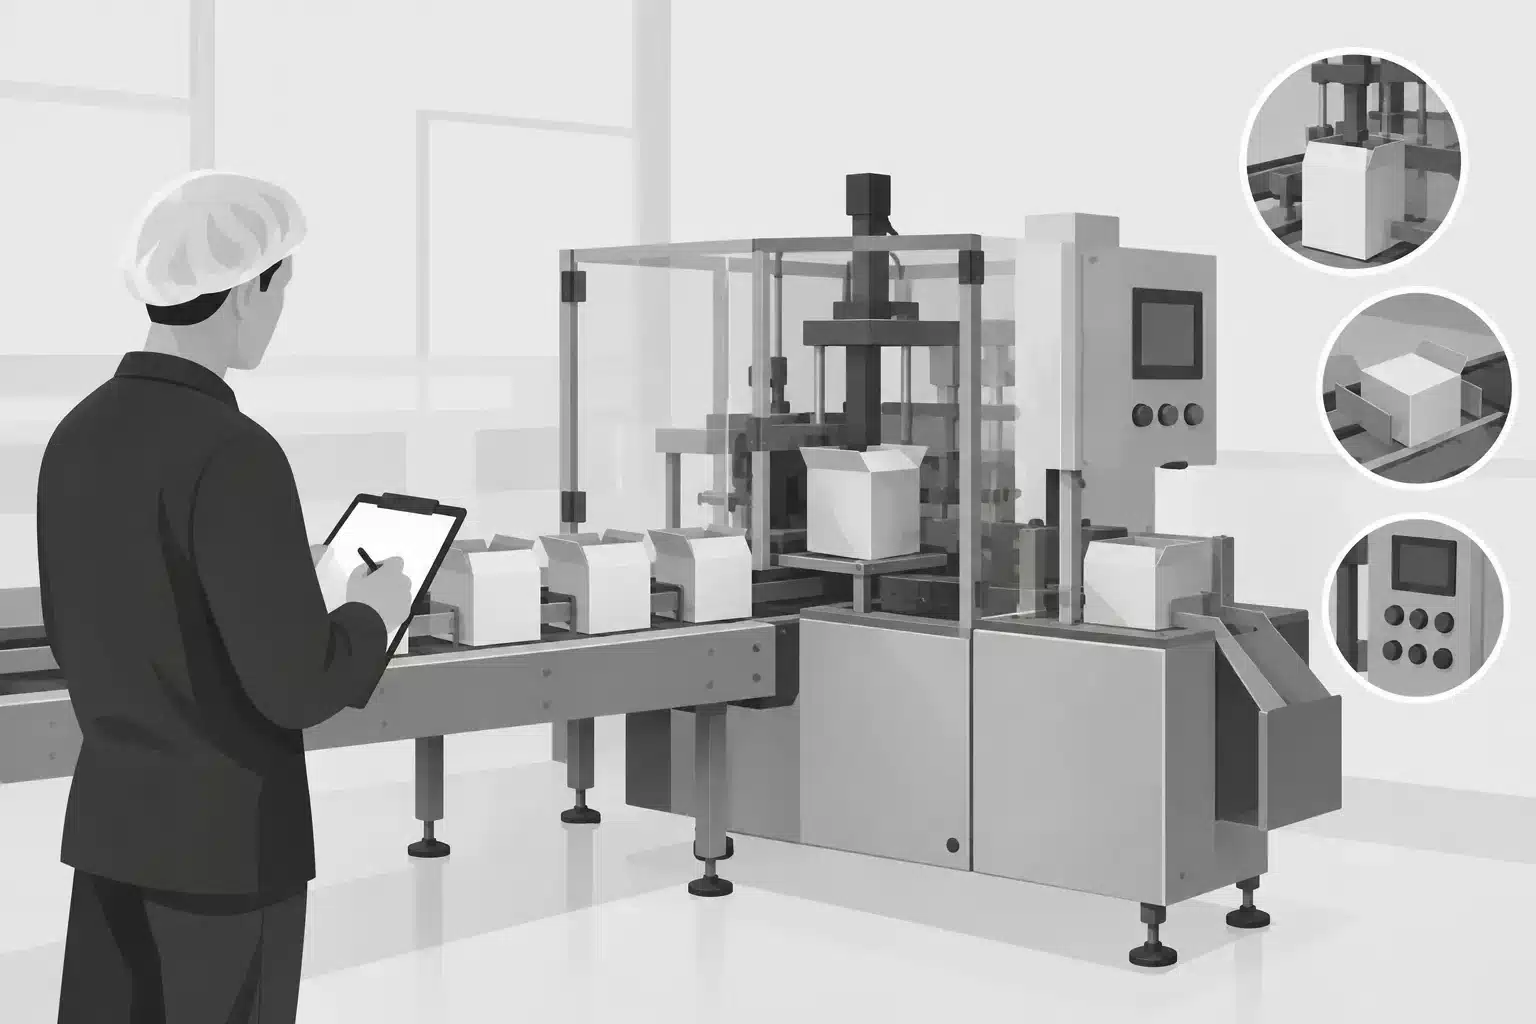
A cartoner can look right on paper and still become the slowest point on the line. The difference is usually in the details: carton range, product presentation, infeed timing, closure style, and how the machine communicates with upstream and downstream equipment. A proper cartoner setup starts with those operating facts, not simply a target speed or a machine model.
For plants buying used equipment, this discipline matters even more. A proven CAM, Langen, ADCO, or similar cartoner can provide excellent value, but it must be configured for the actual product and packaging operation. The goal is not to buy the largest available machine. It is to source a machine that forms, loads, and closes cartons consistently at the required output with practical changeovers and maintainable controls.
Start With the Carton and Product
Carton dimensions establish the working range of the machine. Record the minimum and maximum length, width, and depth of every carton format expected to run. Include the board grade, blank style, print orientation, glue condition, and closure type. A straight tuck carton, reverse tuck carton, glued carton, and five-panel wrap require different handling and tooling considerations.
Product characteristics matter just as much. A cartoner does not package a generic item. It packages a specific product arriving in a specific orientation. That could be a bottle, pouch, tray, blister card, tube, flow-wrapped item, bag, vial, or multipack. Product dimensions, weight, surface finish, temperature, and stability all affect infeed selection and timing.
A bottle that stands reliably may work well with a bucket conveyor or flighted infeed. Loose sachets may require collation before loading. A flexible pouch can need controlled compression or a different carton-loading method to avoid catching flaps. Pharmaceutical or personal-care products may also require inserts, leaflets, lot-code verification, or serialization provisions.
Do not rely on nominal dimensions alone. Provide samples where possible, along with carton blanks and any inserts. Small differences in carton stiffness or product geometry can determine whether a setup is stable or continually needs adjustment.
Define the Required Cartoner Setup Speed
Cartoner speed should be based on sustained production, not the highest number printed on a machine nameplate. If the production line must deliver 120 finished cartons per minute for a full shift, the cartoner needs enough operating margin to maintain that rate through normal variation, minor stops, and material replenishment.
Start with the required net output. Then account for expected reject rates, planned downtime, changeovers, and the output of upstream equipment. A cartoner rated at 150 cartons per minute may be adequate for a 110-carton-per-minute line, but only if the product feed, carton magazine, and discharge equipment support that pace.
The upstream process is often the limiting factor. A filler may run at a variable rate. A labeler may create spacing inconsistencies. A shrink wrapper may deliver products in intermittent groups. The cartoner must receive product in a repeatable pitch and orientation. If it cannot, the issue is not necessarily the cartoner itself. It may be accumulation, metering, collation, or transfer design.
Downstream handling deserves equal attention. Cartons leaving the machine must be accepted without back pressure or damage. Checkweighers, metal detectors, case packers, and conveyors need compatible speeds, elevations, controls, and accumulation capacity. A well-specified cartoner cannot compensate for a poorly matched discharge system.
Match the Machine Style to the Application
Horizontal and vertical cartoners solve different packaging problems. A horizontal cartoner is commonly used when products are loaded from the side into open cartons, including bottles, tubes, trays, pouches, and wrapped products. It can be a strong fit for applications requiring leaflets, product collation, or higher speeds.
Vertical cartoners are often suited to products that can be loaded from above, such as bags, pouches, or certain food products. The right choice depends on how the product arrives, how it must be oriented, and the carton design. Neither style is automatically better.
Intermittent-motion cartoners are practical for many moderate-speed operations and can offer accessible adjustment points for format changes. Continuous-motion machines are built for higher output, but they demand consistent product feed and carton quality. Higher throughput can be valuable, yet it also increases the cost of incorrect timing, worn components, and operator error.
Ask whether the machine needs to handle a single format or a range of SKUs. A dedicated setup can be simpler and faster. A multi-format machine gives flexibility, but it may need change parts, recipe controls, servo adjustments, and more setup time. Plants with frequent SKU changes should evaluate changeover requirements as seriously as maximum speed.
Plan Change Parts and Format Control
Change parts are not accessories. They are part of the machine’s productive capacity. Carton pockets, product buckets, guides, flight attachments, folding rails, and magazine components may all be format-specific. Missing or poorly matched change parts can turn an otherwise capable used cartoner into a costly project.
Before purchasing, build a format matrix. List every product and carton combination, required output, loading method, closure style, and available change parts. Identify which formats can run with adjustment only and which require dedicated tooling. This quickly exposes whether a machine meets the current requirement or only one portion of it.
For frequent changeovers, consider the practical work involved. Are adjustments handwheel-based, mechanical, or recipe-driven? Are settings clearly marked? Can one trained operator complete the changeover, or does it require maintenance support? Older mechanical cartoners can be dependable and economical, but a plant running many short batches may benefit from more repeatable format control.
It also pays to confirm the availability of replacement parts. Established cartoner brands often offer an advantage because components, documentation, and experienced service resources are more accessible. That does not remove the need for inspection, but it reduces long-term ownership risk.
Check Utilities, Controls, and Line Integration
A cartoner setup must fit the plant as well as the product. Confirm electrical requirements, compressed-air demand, machine footprint, infeed and discharge heights, guarding, and operator access. Measure the space needed for carton-magazine loading, maintenance access, and removal of change parts. A machine that physically fits between conveyors may still be difficult to operate safely.
Controls compatibility should be reviewed early. Determine the existing plant voltage, control architecture, communication needs, safety circuit requirements, and preferred components. If the line uses Allen-Bradley controls and the cartoner has an obsolete platform, the machine may still be usable, but the upgrade cost and support plan should be understood before delivery.
Product and carton detection also need to match the application. Photo eyes, no-product/no-carton logic, carton-open detection, reject verification, and code-reading systems each serve a purpose. Regulated applications may require more detailed validation and documentation than general consumer-goods packaging. Specify that requirement at the beginning, not after the machine has been selected.
Evaluate Used Equipment on Operating Evidence
Used cartoners are not equal simply because they share a brand name and approximate age. Condition depends on prior application, maintenance history, stored environment, available tooling, controls condition, and whether the machine can be demonstrated with representative materials.
A useful evaluation looks beyond cosmetics. Inspect the carton magazine, vacuum system, chains, drives, bearings, gearboxes, folding mechanisms, glue components where applicable, safety guards, electrical enclosure, and HMI. Verify that the machine cycles correctly and that cartons are erected, loaded, closed, and discharged consistently. If a product trial is possible, it provides far more value than an unloaded dry cycle.
Documentation matters. Electrical drawings, manuals, spare-parts lists, and change-part records can reduce installation time and simplify maintenance. Ask what is included with the machine, what has been tested, and what work is recommended before commissioning.
Mectec Packaging Machinery focuses on sourcing and evaluating used packaging equipment so buyers can make decisions based on application fit and machine condition, rather than limited listing details alone.
Common Setup Errors That Create Downtime
Most cartoner problems are predictable. The recurring issue is a mismatch between the machine’s intended operating window and the real production environment. Watch for these four failures:
- Selecting by maximum speed while ignoring sustained output and line accumulation.
- Assuming all cartons within a stated size range will run without format-specific tooling.
- Treating product presentation as a conveyor issue instead of a cartoning requirement.
- Buying a machine before confirming utilities, controls, guarding, and available floor space.
Each error can be corrected, but correction after delivery is slower and more expensive. Good specification work shifts those decisions ahead of procurement, where they belong.
The right cartoner is the one that handles your actual cartons and products reliably, fits the line, and can be maintained without constant intervention. Define the application precisely, verify the machine against it, and leave enough room in the plan for changeovers, service access, and real production conditions.