A checkweigher that drifts by only a few grams can create a costly problem fast. Underweight packs expose the operation to compliance risk and customer complaints. Overweight packs quietly consume margin on every run. Reliable checkweigher calibration steps turn the machine from a simple reject device into a dependable control point on the packaging line.
The correct procedure depends on the checkweigher model, product weight range, belt configuration, and the standards governing the product. The machine manufacturer’s manual and site quality procedures should always control. Still, the operating principles are consistent across most in-motion systems used in food, beverage, pharmaceutical, personal-care, and consumer goods production.
Start with the conditions around the machine
Calibration begins before a test weight touches the infeed belt. A checkweigher measures force while a product is moving, so mechanical condition and line stability matter as much as the settings on the screen.
Make sure the system is level and firmly supported. Inspect the infeed, weigh belt, and discharge conveyor for belt damage, buildup, loose hardware, worn bearings, or belt tracking issues. Product guides should be secure without contacting or rubbing the package during its trip across the weigh section. A guide that applies pressure to a carton can produce unstable readings that look like a load-cell issue.
Clean the weigh conveyor and remove trapped film, product debris, moisture, or loose labels. Confirm that the machine is isolated from nearby vibration where possible. Equipment such as fillers, compressors, case packers, and conveyors can transmit vibration through a shared frame or floor. If the readings fluctuate with no product present, investigate the environment before changing calibration values.
Let the checkweigher warm up according to the OEM’s recommended period. Electronic components and load cells can shift slightly as they reach operating temperature. Calibrating immediately after startup, then running production for eight hours, can result in a system that was accurate only at the moment it was adjusted.
Checkweigher calibration steps for a controlled test
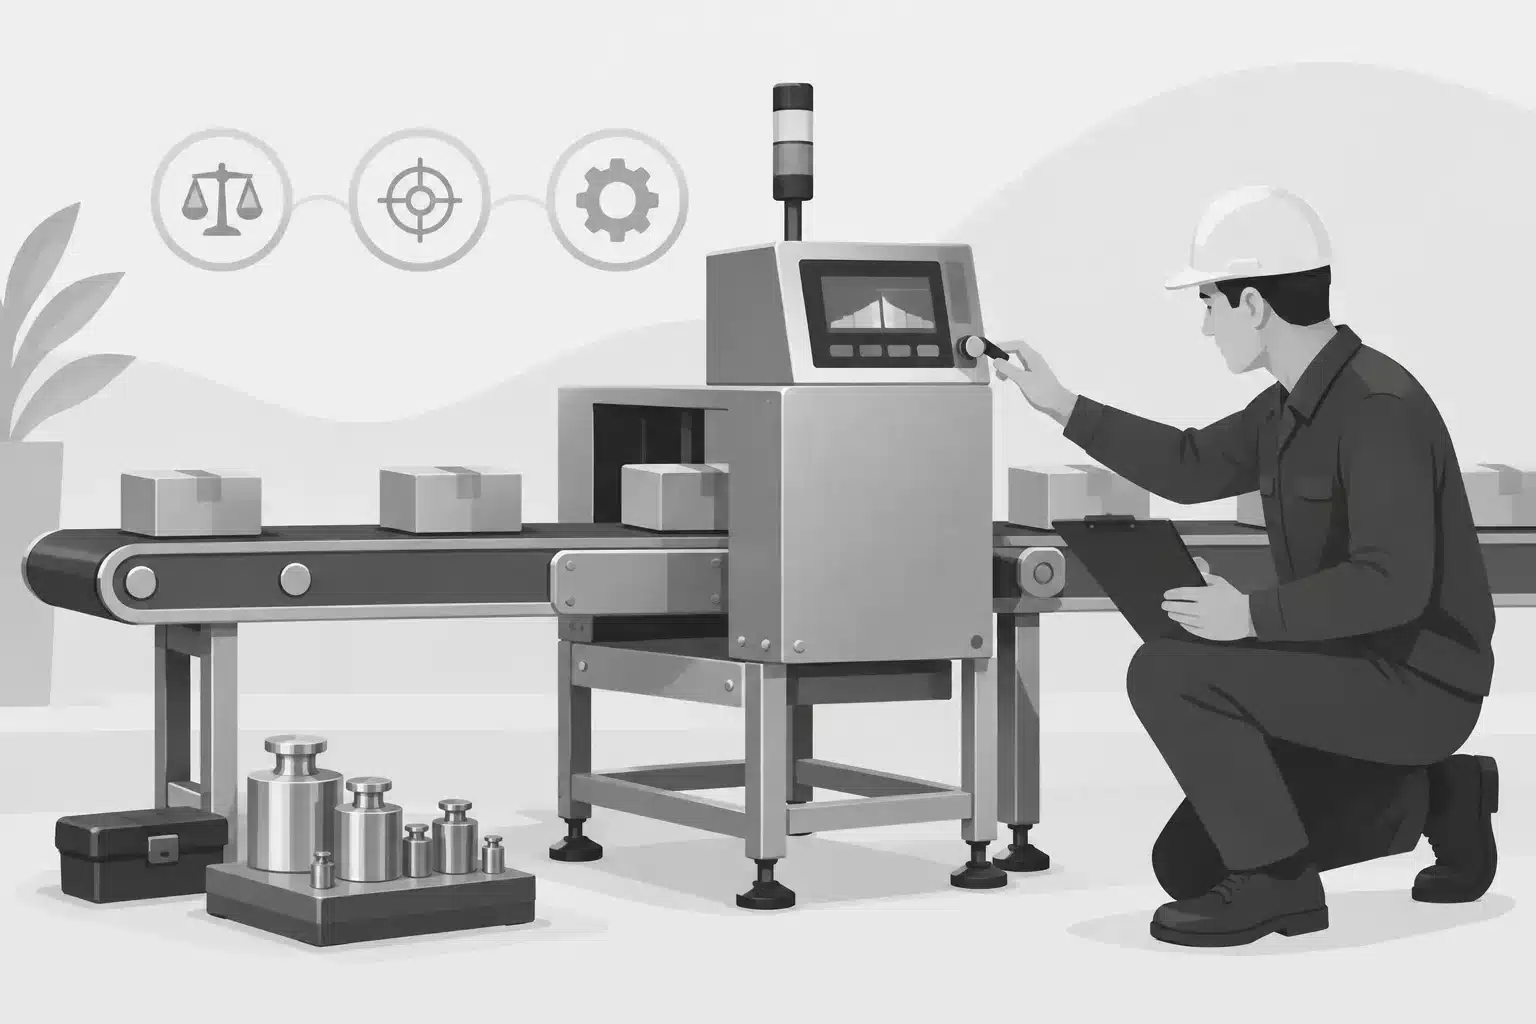
Begin with the machine empty and stopped or in its prescribed calibration mode. Zero the scale only after confirming that nothing is contacting the weigh belt. The zero value establishes the baseline for every subsequent measurement. If zero will not hold, do not compensate by repeatedly re-zeroing. Inspect for debris, mechanical interference, vibration, cable damage, or a failing load cell.
Next, use certified or traceable test weights appropriate for the machine’s capacity and expected product range. A 500-gram test weight may be useful for a 500-gram product, but it does not fully prove performance for a line that also runs 50-gram sachets or 2-kilogram packs. Select weights and test points that reflect the actual operating window.
Place the test weight on the weigh belt as directed by the manufacturer. For static verification, position and placement are usually controlled closely. For dynamic calibration, send the test weight through at the normal production speed and spacing. An in-motion checkweigher is calibrated for a moving process, not just a stationary load.
Enter or confirm the known reference value, then allow the controller to calculate the adjustment where the OEM procedure calls for it. Record the before-and-after readings, the test-weight identification, date, time, operator, product program, line speed, and any correction made. This record is what allows quality and maintenance teams to distinguish a one-time adjustment from a recurring issue.
Calibration at a single point is not always enough. Verify zero, a lower-range point, a nominal product-weight point, and, when applicable, an upper-range point. The number of points and tolerance limits should follow the OEM specification and the facility’s quality plan. More points improve confidence, but only if they are relevant to the products being run and can be performed consistently.
Verify performance with real production conditions
A test weight confirms the measuring system. It does not necessarily confirm that the line can handle actual packages. Product shape, unstable contents, package finish, spacing, and transfer timing can all affect an in-motion result.
Run representative production samples at normal line speed after calibration. Use samples that have been independently verified on a suitable reference scale. Observe the checkweigher’s displayed values and compare them with the reference values. Repeat the test enough times to reveal variation rather than relying on one favorable pass.
Check package spacing and transfer. Products must enter the weigh belt cleanly, without touching the preceding or following package. A fast line with inconsistent pitch may need a timing adjustment, metering improvement, or a lower operating speed. Calibration cannot correct poor product separation.
Then verify the reject system. A properly calibrated checkweigher still fails its purpose if an out-of-tolerance package reaches the case packer. Test underweight and overweight samples, where permitted by site procedures, and confirm that each reject is positively removed, accounted for, and handled according to the line’s reject confirmation requirements. For regulated applications, reject verification and recordkeeping may be as critical as the displayed weight.
Set tolerances for the product, not convenience
Target weight, warning limits, reject limits, and control limits should reflect the product specification, legal requirements, filler capability, and normal process variation. They should not be widened simply to reduce rejects.
A narrow tolerance can generate excessive false rejects if the upstream filler has ordinary variation or the package is difficult to weigh dynamically. A wide tolerance may reduce rejects while allowing too much giveaway or creating risk at the low end. The workable setting is the one that protects the declared net content while giving operations useful feedback about the filling process.
Use checkweigher data to identify trends. A steady movement toward overweight production often points to filler drift, temperature effects, ingredient changes, or a deliberate safety margin that has become too large. A growing spread in weights may indicate inconsistent filling, package handling problems, or wear in the checkweigher itself. The checkweigher should trigger investigation, not become the place where upstream problems are hidden.
Build a calibration frequency that matches risk
There is no universal interval for calibration. A lightly used checkweigher on a stable dry-goods line may need a different schedule than a high-speed system operating through multiple shifts in a washdown environment. Product risk, regulatory requirements, production volume, historical performance, and OEM recommendations all matter.
Many operations combine a formal calibration interval with routine verification checks. Verification may occur at startup, after product changeover, after maintenance, after a jam or belt replacement, and at scheduled intervals during a long run. Calibration is the controlled adjustment of the instrument. Verification is evidence that it remains accurate. Treating both as the same task leaves gaps in control.
Investigate immediately if the system fails verification, requires frequent adjustment, or shows unstable repeatability. Common causes include load-cell damage, contaminated or worn belts, incorrect belt tension, misaligned transfers, loose frames, electrical noise, poor grounding, and vibration. Replacing a component without identifying the underlying condition can make the problem return on the next shift.
Keep the machine serviceable
Checkweigher accuracy is easier to maintain when service items are not allowed to become production emergencies. Keep the weigh belt clean and correctly tensioned. Inspect idlers, bearings, product guides, transfer plates, and reject hardware during planned maintenance. Protect load-cell cables from pulling, pinching, and washdown damage. When a belt, load cell, controller, or conveyor component is replaced, complete the required calibration and documented verification before releasing the line.
For used equipment, ask for more than a statement that the checkweigher powers on. Confirm the capacity, belt dimensions, product-handling arrangement, reject method, controller condition, available manuals, and whether suitable test weights and calibration documentation are included. A unit that fits the line mechanically but cannot provide repeatable results at the required speed is not a cost-saving purchase.
Mectec Packaging Machinery helps buyers evaluate used packaging equipment against the actual application, including product format, line speed, and integration requirements. That focus reduces uncertainty before a machine reaches the plant floor.
A disciplined calibration routine protects product, margin, and uptime. Keep the procedure controlled, test the machine under real operating conditions, and treat unexplained drift as a maintenance signal worth acting on.